


Jan. 01, 1970
Choosing a patterned leisure shirt supplier is not simply a matter of selecting the brightest artwork. A retailer needs to balance fabric feel, print durability, minimum order quantity, color accuracy, and delivery risk. This guide evaluates custom patterned leisure shirts, wholesale sublimation leisure shirts, and the best polyester shirts for all-over printing through practical production details. It also explains dye sublimation printing, moisture-wicking polyester, all-over print apparel, CMYK color management, vapor-phase dye transfer, and GSM fabric weight, so buyers can decide whether sublimation suits their customers, order size, and sales channel.

A shirt may look impressive on a product screen and still create problems after production. A white polyester base can make colors appear clean, while an unsuitable cotton blend may produce a weak or incomplete transfer. A design that looks centered on a flat template can also shift across the collar, side seam, or button placket. These issues affect returns, customer reviews, and the cost of reprinting.
Sublimation deserves a complete review because it changes both the appearance and the manufacturing workflow. The process is excellent for detailed patterns and small-batch customization, but it depends on polyester content, heat stability, file preparation, and supplier quality control. Meninthemirror and other apparel suppliers should therefore be assessed not only by catalog photos, but also by fabric specifications, pre-production samples, color approvals, and documented inspection procedures.
In dye sublimation printing, solid dye particles are printed onto coated transfer paper and then heated under controlled pressure. At approximately 180–205°C, the dye changes into a gas and bonds with polyester fibers. The printed paper is removed after cooling, leaving the color inside the fiber rather than forming a thick layer on top.
The exact temperature, dwell time, pressure, and fabric construction vary by printer, heat press, ink system, and shirt design. Many production settings fall within roughly 180–205°C for about 45–60 seconds, but a supplier should validate the settings with its own equipment. These figures are process ranges, not a guarantee that every shirt will perform identically.
This method differs from screen printing and direct-to-garment printing. Screen printing places ink layers on the surface and can be economical for large quantities with limited colors. Direct-to-garment printing is more flexible for cotton garments but may show a different hand feel and wash response. Sublimation is most effective when the buyer wants an edge-to-edge image on a white or light-colored polyester shirt.
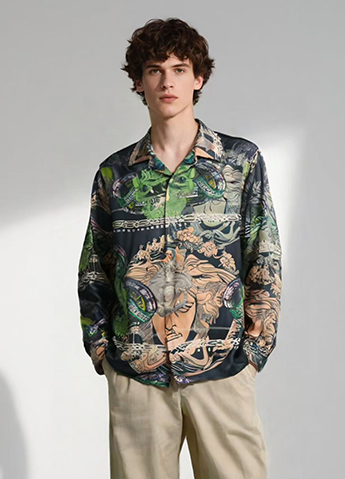
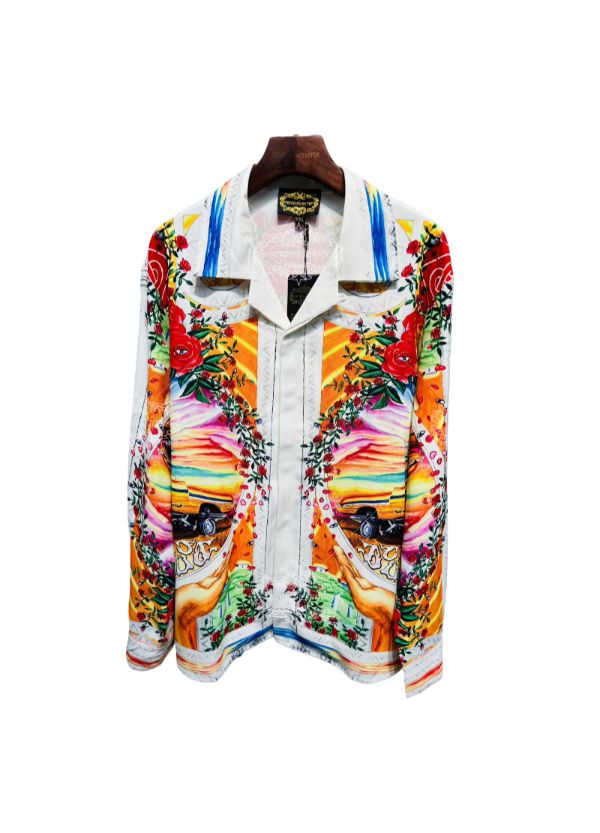
The main advantage is design coverage. A sublimation file can continue across the front, back, sleeves, and selected side panels, allowing a brand to create florals, geometric repeats, gradients, photographic images, or event graphics. The design is not restricted to a small chest or back print.
For a business selling resort shirts, team apparel, travel clothing, or limited collections, this coverage supports a stronger visual identity. A repeating pattern can also reduce the need for separate front and back artwork, although the pattern still needs careful placement around seams and pockets.
Sublimation can reproduce fine lines and multicolor artwork without the raised ink layer associated with some surface-printing methods. It is suitable for gradients, small decorative elements, and complex illustrations when the printer uses an appropriate ICC profile, calibrated equipment, and consistent transfer paper.
Color should not be judged from a monitor alone. Screens use RGB light, while most commercial dye-sublimation workflows convert artwork through CMYK-based color management or a printer-specific color profile. Neon shades, metallic effects, and extremely saturated colors may shift because the printable gamut is limited. A physical strike-off remains more reliable than a digital proof.
Sublimation can be practical for test collections because the artwork is digitally prepared rather than separated into multiple screens. In some factories, small orders may begin at approximately 10–50 pieces per design, while larger suppliers may require higher quantities for custom fabric, labels, or special packaging. The actual minimum order quantity must be confirmed before sampling.
This flexibility allows a retailer to test several patterns instead of committing all capital to one design. A sensible pilot might compare three patterns in two sizes, then reorder the design that achieves the strongest sell-through. The financial benefit comes from lower initial inventory exposure, not from assuming that the per-piece price will always be lower.
Because the dye enters the polyester fiber, the finished area generally does not have a separate rubbery ink film. This can help preserve a smooth hand feel across a large printed surface. The design is also less likely to crack in the same way a thick surface print can crack after repeated flexing.
That does not make the garment indestructible. Fabric abrasion, heat damage, chemical exposure, seam stress, and poor washing practices can still reduce appearance. A quality assessment should include wash testing and a review of the fabric itself, not only the print surface.
Many sublimated leisure shirts use polyester because the fiber accepts the dye. Polyester can also dry faster than cotton under comparable conditions because it absorbs less liquid into the fiber. However, drying time depends on fabric thickness, knit structure, airflow, humidity, and garment construction. A supplier should provide fabric composition and GSM fabric weight rather than relying on phrases such as “quick dry.”
For warm-weather shirts, a lightweight fabric around 120–160 GSM may feel cooler than a heavier 180–220 GSM fabric, but a lower GSM can also reduce opacity, structure, and durability. These are general manufacturing ranges rather than universal quality grades. A buyer should request a sample in the exact fabric planned for bulk production.
Sublimation works best on white or light polyester. The process adds dye but does not provide an opaque white layer, so it cannot reliably turn a dark black, navy, or red shirt into a bright base for a pale design. A dark garment will usually suppress or alter the printed colors.
There are practical alternatives. The supplier may use white polyester fabric before cutting and sewing, select a light-colored base, or recommend screen printing, heat transfer, or another method for dark garments. The choice should be made before the pattern is finalized because changing the print method can require a new file, sample, price, and production schedule.
Pure or high-percentage polyester normally produces the most predictable sublimation result. Polyester blends can work, but the non-polyester fibers may remain unprinted or create a faded, heathered, or less saturated appearance. For example, a 65% polyester and 35% cotton fabric cannot be expected to look identical to a 100% polyester fabric using the same artwork and press settings.
Ask for the exact fiber ratio, fabric construction, finish, and shrinkage information. If a soft cotton-like touch is essential, a blended fabric may be attractive, but the buyer should approve a physical sample because softness and color intensity can conflict.
The transfer process exposes the fabric to temperatures near 180–205°C. Heat-sensitive finishes, unstable knits, elastane, and poorly prepared fabric may shrink, develop a shiny press mark, or lose dimensional accuracy. Lightweight fabrics can also show seam impressions or slight edge distortion after pressing.
Suppliers can reduce these risks through pre-shrunk fabric, calibrated pressure, protective paper, test pressing, and pattern compensation. Buyers should measure the sample before and after washing and compare key points such as chest width, body length, sleeve length, and collar opening. A tolerance of approximately ±1–2 cm is common in apparel production, but the permitted range must be agreed in the purchase specification.
An all-over design rarely joins perfectly at every seam. Differences of a few millimeters can occur because of fabric stretch, cutting tolerance, sewing movement, or panel registration. Stripes, grids, large faces, and straight lines make these differences more visible than small floral or abstract patterns.
To reduce complaints, send the supplier a panel-based technical file, identify the front center, back center, sleeve direction, and seam matching points, and request a sewn sample rather than approving a flat printed panel alone. Pockets, collars, buttons, and plackets should be shown in the artwork proof because they can interrupt the pattern.
Two production lots may show slight differences when fabric batches, ink batches, paper, humidity, or machine calibration changes. The same RGB color displayed on two monitors may also appear different on fabric. A buyer should approve a physical color standard and define an acceptable tolerance using a supplier’s available measurement system, such as spectrophotometer readings where applicable.
Do not approve color solely from a screenshot. If a specific brand color is commercially important, provide a physical reference or a recognized color standard and state whether the requirement applies to the printed panel, finished garment, or both.
The dye is embedded in the polyester fiber, but garment care can still affect color and fabric condition. Washing at a moderate temperature, turning the shirt inside out, using a mild detergent, and avoiding chlorine bleach can reduce unnecessary stress. High heat from tumble drying or ironing may damage synthetic fabric even when the print itself remains stable.
Care labels should match the tested garment. A supplier should not promise a fixed number of washes without defining the test method, detergent, temperature, cycle, and pass-fail criteria. A practical quality program may compare appearance after 5, 10, or more standardized wash cycles, but the result depends on the fabric and construction.
Record the intended use, target retail price, size range, fabric composition, GSM, fit, collar type, sleeve length, pocket position, buttons, labels, and packaging. A resort shirt, a sports shirt, and a casual overshirt may all be called leisure shirts, but they require different fabric weights and construction details.
Also decide whether the design must cover only the main body or continue onto sleeves, collar, placket, and pocket flaps. This decision affects the pattern template, fabric consumption, cutting process, and final quote.
Use the supplier’s actual panel templates instead of placing artwork on a generic shirt outline. Confirm document dimensions, bleed, seam allowance, front and back orientation, sleeve direction, and file format. Raster artwork should be supplied at a resolution appropriate to the final size; many production teams request approximately 150–300 pixels per inch at actual output size, but the supplier’s specification should take priority.
Keep editable source files, embedded fonts, linked images, color references, and a flattened preview. Large faces, text, and geometric lines require extra placement attention because even a small shift can be noticeable after sewing.
Approve more than a loose fabric swatch. A sewn sample reveals collar placement, seam alignment, button position, drape, opacity, fit, and how the pattern behaves when worn. Measure the garment, photograph it under neutral lighting, and compare it with the approved artwork.
For a commercial order, examine at least one sample after washing. Check color, shrinkage, seam puckering, fabric hand, odor, loose threads, button attachment, and print coverage. If the shirt is intended for outdoor or frequent-use customers, add abrasion and light-exposure testing appropriate to the product claim.
Separate one-time costs from unit costs. Ask whether the price includes artwork adjustment, sample production, fabric, labels, buttons, packaging, inspection, and delivery. Confirm the minimum order quantity by design, colorway, size, and fabric.
Request a written tolerance for measurements, color variation, print registration, defects, and quantity shortage. These terms are more useful than a general promise of “high quality” because they create an objective basis for inspection.
Use a statistically based inspection plan or an agreed sample size rather than checking only the first and last shirts. At minimum, inspect artwork orientation, major stains, pinholes, seam defects, collar symmetry, button security, measurements, labels, and packaging. For repeated patterns, inspect areas where misalignment is most visible.
If the order is large, retain approved samples from the same production lot. They provide a reference if a customer reports color or construction differences later.
Sublimation is usually a strong option when the product uses white or light-colored polyester, requires edge-to-edge artwork, includes many colors, and will be produced in small or medium design runs. It is particularly suitable for custom collections, resort wear, event shirts, team apparel, and limited releases where visual variety matters more than a natural cotton fiber content.
It is less suitable when the shirt must be made from dark cotton, when a specific opaque base color is essential, or when the buyer cannot tolerate small registration differences at seams. In those cases, screen printing, direct-to-garment printing, heat transfer, yarn-dyed fabric, or a different garment construction may produce a more predictable result.
The decision should be based on total landed cost rather than the print price alone. Include sampling, artwork preparation, fabric waste, freight, inspection, rework, returns, and inventory risk. A lower unit quote can become expensive if the fabric is too thin, the color is inconsistent, or the first shipment cannot be sold at the planned price.
Choose sublimation if your priority is a detailed all-over pattern on a light polyester base and you can approve a physical sample before placing the bulk order. Specify the polyester ratio, GSM fabric weight, finished measurements, color standard, seam tolerance, care label, and inspection criteria. For the first order, use a controlled quantity and test customer response before expanding the range.
Work with a supplier that can explain its dye sublimation printing settings, provide a sewn pre-production sample, identify its CMYK color management process, and document how it checks moisture-wicking polyester, shrinkage, and seam alignment. Meninthemirror can be considered alongside other suppliers, but the final choice should depend on verified samples and written production controls rather than brand presentation alone.
Sublimation offers edge-to-edge color, a smooth printed hand, detailed artwork, and flexible design testing, but it requires light polyester, disciplined color control, and realistic expectations about seam registration and heat-related changes. It is not a universal replacement for every printing method. For retailers seeking custom patterned leisure shirts or wholesale sublimation leisure shirts, the safest route is to test the best polyester shirts for all-over printing in the exact fabric, validate dye sublimation printing, document moisture-wicking polyester and GSM fabric weight, and approve the final garment before production. With that process, sublimation can be a commercially sound choice for patterned leisure shirts; without it, attractive artwork may not translate into a dependable product.
Latest News
Top Print Finishes for Premium Baroque Graphic Tees
When a baroque t-shirt manufacturer turns an ornate artwork into a premium garment, the difficult part is rarely the design alone. Fine scrollwork can disappear into cotton fibers, metallic ink can crack after washing, and a dark shirt can shift the colors of a palace-inspired graphic. For brands searching for premium baroque graphic tees with metallic foil, the best print finish for ornate
Jan. 01, 1970
Gallery Tee Print Review: Sharpness, Hand Feel, and Wash Resistance
Looking for a gallery t-shirt manufacturer that can produce a clean men gallery tee shirt without a stiff print or early cracking? This gallery tee shirt print review examines the best gallery t-shirt for men through three practical questions: does the artwork retain fine detail, does the print feel comfortable against the skin, and does it survive repeated washing? The review covers screen
Jan. 01, 1970
Pros and Cons of Sublimation for Patterned Leisure Shirts
Choosing a patterned leisure shirt supplier is not simply a matter of selecting the brightest artwork. A retailer needs to balance fabric feel, print durability, minimum order quantity, color accuracy, and delivery risk. This guide evaluates custom patterned leisure shirts, wholesale sublimation leisure shirts, and the best polyester shirts for all-over printing through practical production
Jan. 01, 1970
Let's Take This Forward!
Feel free to reach out for any queries. We would be happy to help!

